01
Cold aggregate bin feeder
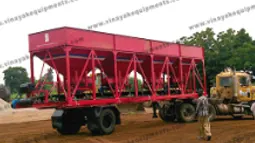
Four bins (100–150 t heaped storage on drum plants) fitted with bin vibrators and auxiliary conveyors meter each aggregate size onto a gathering conveyor.
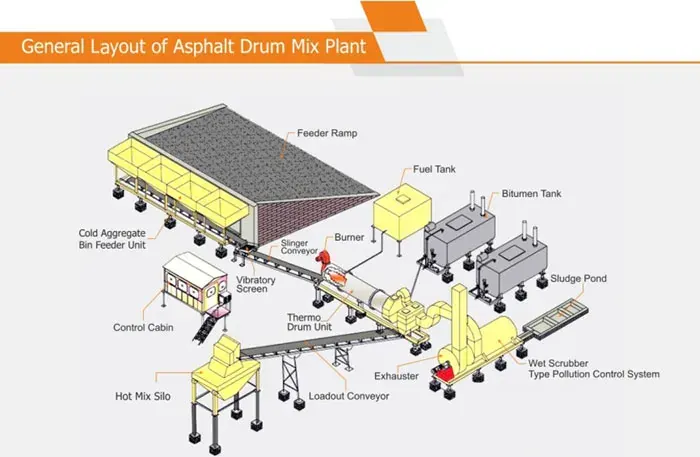
A clear guide to every unit in a Vinayak asphalt drum mix plant, from the cold feeder to the control cabin, with the sizes used on each model.
The plant is a line of units: aggregate enters at the cold feeder and leaves as hot mix at the load-out conveyor. Bitumen, fuel and filler join from the side. The control cabin watches the whole line. Knowing each component helps you compare quotations properly and plan maintenance.
Looking for the complete plant? See the asphalt drum mix plant and asphalt batch mix plant pages.
Four bins (100–150 t heaped storage on drum plants) fitted with bin vibrators and auxiliary conveyors meter each aggregate size onto a gathering conveyor.
A continuous electronic belt weighing system with load cell measures the aggregate feed. A vibratory screen with 45 mm openings removes oversize before the drum.
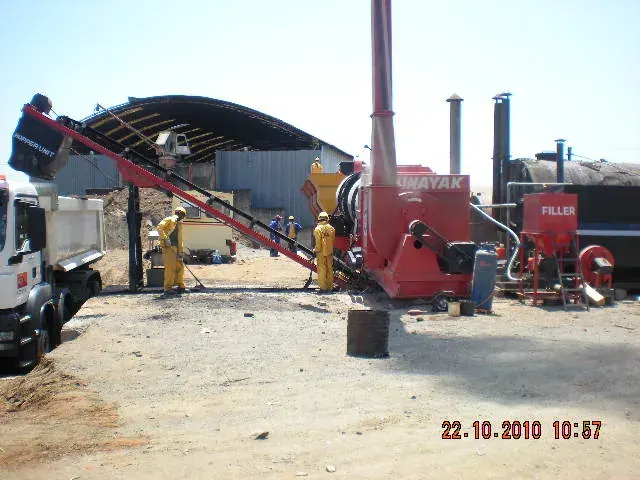
A high-speed conveyor throws the screened aggregate into the drum inlet, sized from 500 to 600 mm belt width depending on model.
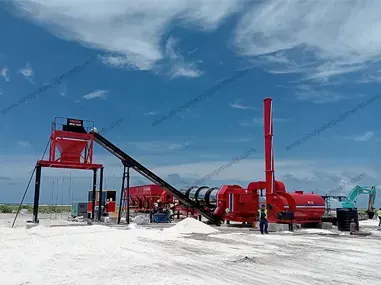
The heart of a drum mix plant. A glass-wool insulated drum of 1200–1800 mm diameter, with cradle chain drive, dries, heats and then coats the aggregate with bitumen.
High-pressure, fully automatic dual-stage diesel burner (350–750 LPH on drum plants; modulating 6.5–13.6 MW on batch plants), with blower and pumping station.
A multi-clone primary collector captures coarse dust. A secondary venturi wet scrubber (below 150 mg/m³) or reverse-air bag house (below 50 mg/m³) handles fines.
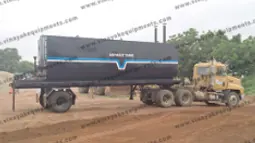
U-shaped, fully insulated tanks of 15–25 t on drum plants, with direct heating and a metering pump. Batch plants offer 15–50 t tanks with direct or hot-oil heating.
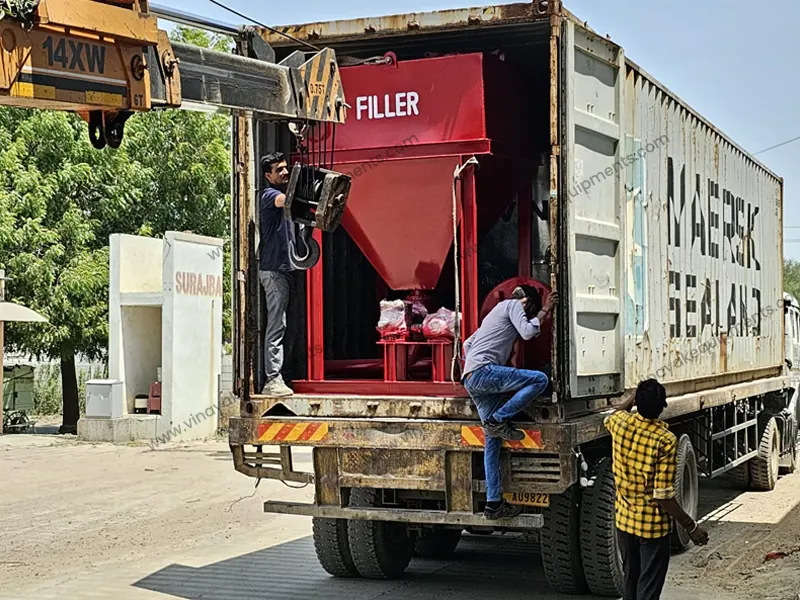
A hopper with worm-gear drive and 150 mm rotary valve doses cement or stone dust filler into the mix.
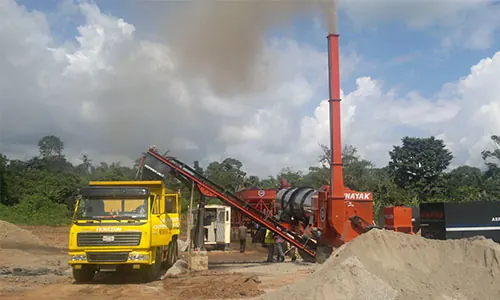
A heat-resistant 600 mm belt carries hot mix to a 1.0–1.5 t hopper with hydraulic gate for truck loading.
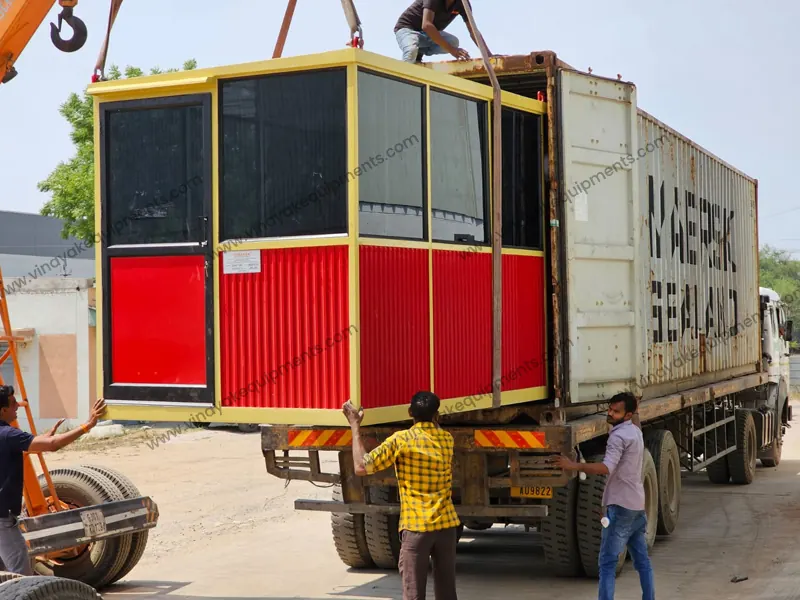
An enclosed cabin houses the SCADA/PLC panel with touch-screen HMI and print-out of production data, so one operator controls the whole plant.
A 3000–5000 L diesel tank, 5.5 kW air compressor and a recommended 100–125 KVA generator set support the plant.
When buyers search for an "asphalt mixer machine", they usually mean the part of the plant where bitumen meets aggregate. In a drum mix plant that is the rear section of the thermo drum, where coating happens continuously. In a batch plant it is a separate twin-shaft, hot-oil jacketed pugmill that mixes 1000–2000 kg per 45-second batch. Both are built by Vinayak as part of a complete plant.
For a step-by-step view of how these components work together, read how an asphalt drum mix plant works.
Cold aggregate bin feeder, vibratory screen, slinger conveyor, thermo drum, dryer burner, dust collector, bitumen tank, fuel tank, mineral filler unit, load-out conveyor and control cabin with SCADA/PLC panel.
Aggregate proportioning (cold feeder and belt weigher), drum heating (burner and drum design) and bitumen metering all affect quality. The control system ties them together so ratios stay consistent.
Contact the team with your plant model and the component you need, and they will confirm availability and pricing.
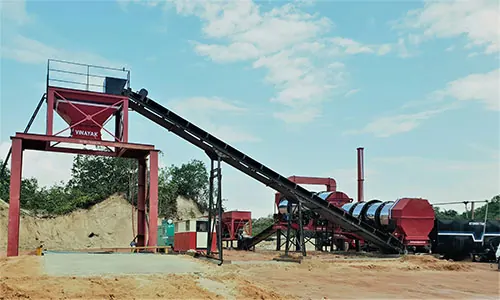
Continuous drum-mix plants in DM-45, DM-50 and DM-60 models, 40 to 120 TPH, stationary or mobile.
View models & specifications →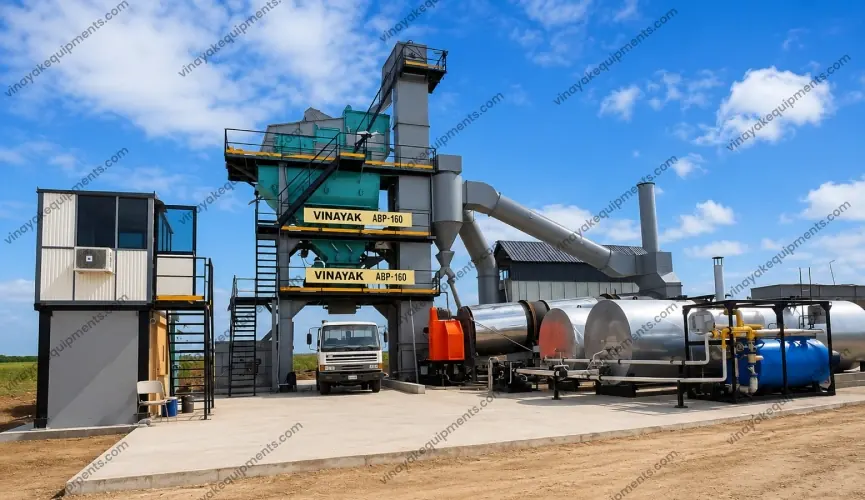
ABP-80, ABP-120 and ABP-160 batch plants with hot screening, weigh bins and twin-shaft pugmill.
View batch plant specs →Step-by-step working principle, from cold feed to load-out, plus applications and advantages.
Read the guide →Share your required output, mix type and site location. The Vinayak team will recommend a model and send a quotation.
